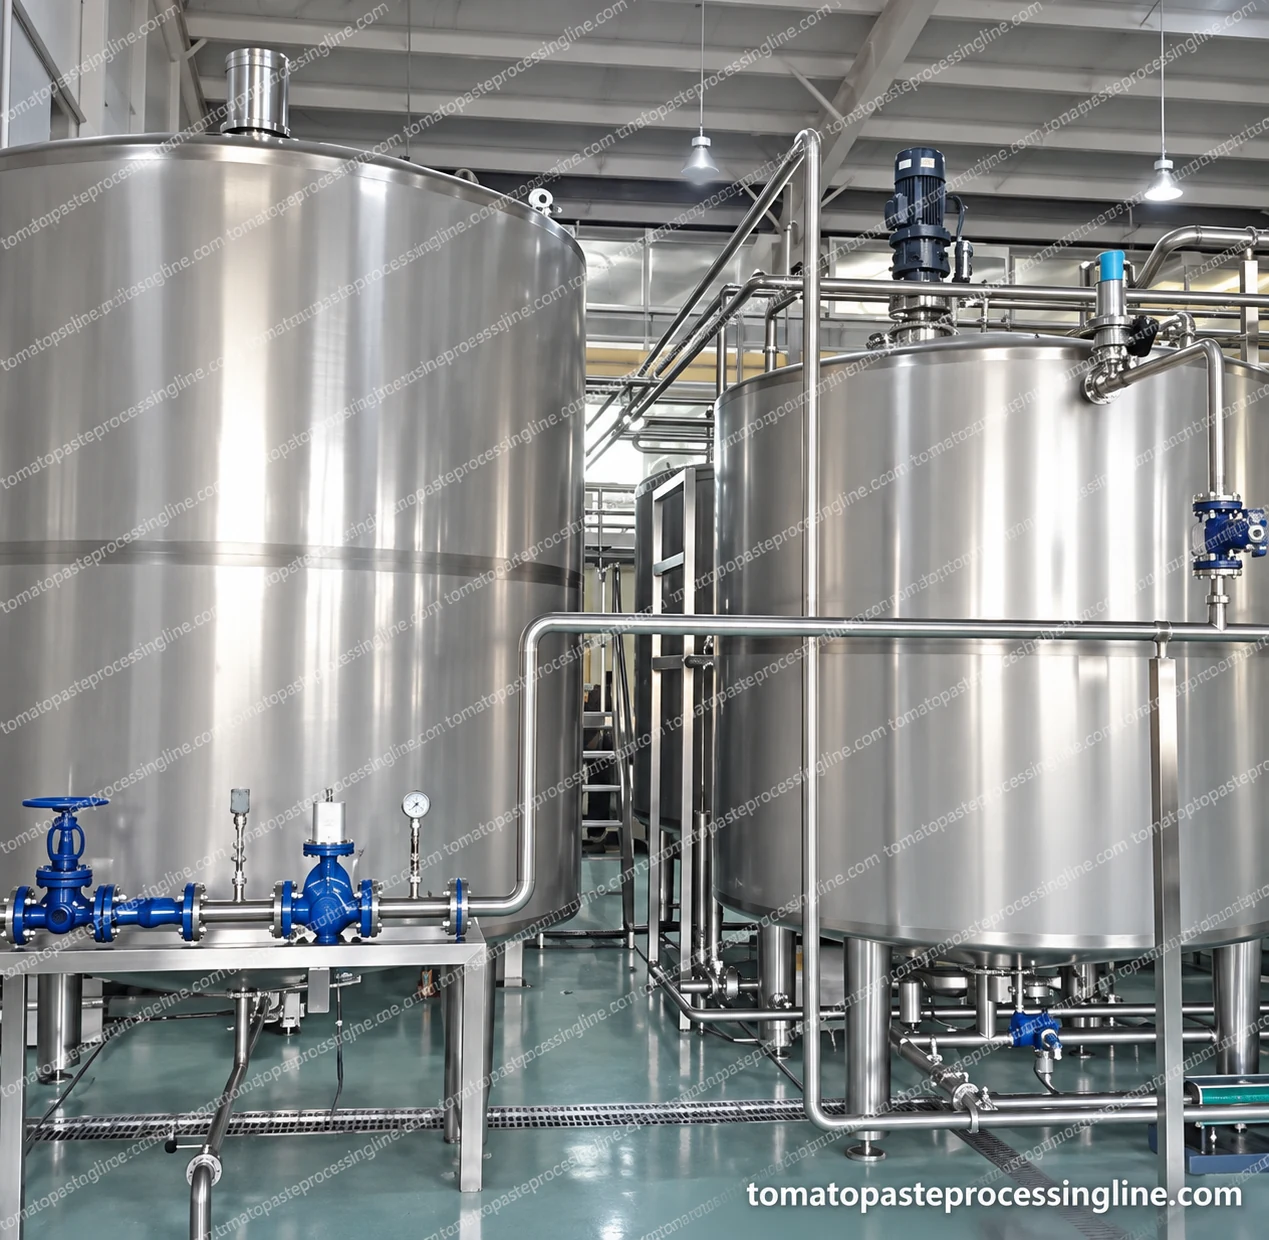
Define useful working volume, not only vessel size
A buffer can separate changes in upstream supply from the immediate needs of the next machine. Its useful working range depends on the intended flow, level-control strategy and the interruption that it is meant to absorb. Gross vessel volume is not the same as usable process capacity.
State whether the material is refined pulp, concentrated paste or a formulated product. The viscosity, temperature and desired operating condition affect transfer and circulation choices. Do not treat all tomato streams as interchangeable when assigning a tank and pump duty.
Coordinate levels and adjoining-machine responses
Level changes should lead to a defined response in upstream feed and downstream transfer. A low level, high level or packaging interruption can affect more than one machine. The operating description should explain how the section stops, resumes and handles retained material.
During concentration, a stable supply can support the selected evaporator operating point. After concentration, outlet pumping and final thermal processing must stay coordinated with filling. A buffer does not remove the need to define those process interfaces or the consequences of a prolonged stop.
Include recovery, drainage and access
The transfer layout should show low points, recoverable product and routes used at startup or shutdown. Retained material influences useful output and cleaning requirements. Check the flow path as a connected system rather than selecting each pump only from a nominal flow number.
Leave access to pumps, instruments, connections and removable components. Closed product routes need appropriate cleaning supply and return interfaces, while external tank and machine surfaces need physical access. Include these requirements in the layout and equipment enquiry.
Further detail
Questions about this equipment and process
Does a larger tank automatically improve continuity?
No. Working range, level control, retained product and the expected interruption should determine buffer duty.
Can a pulp transfer pump be selected without the product condition?
Product temperature, viscosity, flow and adjoining equipment conditions are essential inputs to selection.